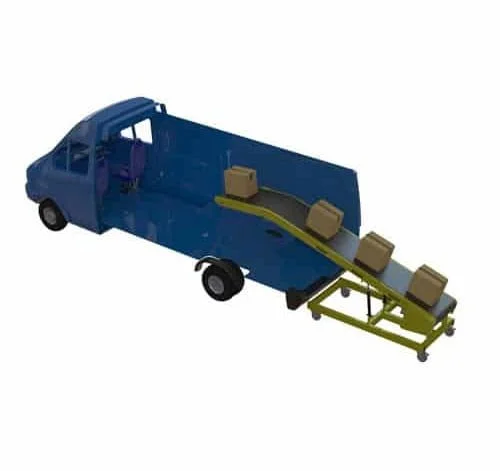
In the rapidly evolving industrial landscape, the efficiency of material handling systems is paramount. Belt conveyors play a critical role in enhancing the efficiency of operations by providing a reliable and effective means of transporting materials. This article delves into some of the top belt conveyor designs that are instrumental in achieving optimal operational efficiency. By exploring cutting-edge designs and configurations, businesses can significantly improve their productivity while minimizing downtime and operational costs.
Innovative Conveyor Design Features
Modern belt conveyor systems incorporate a variety of features that enhance their functionality and efficiency. Understanding these features can help businesses choose the most suitable design for their specific needs.
- Modular Design: Modular belt conveyors allow for easy customization and scalability. They can be easily reconfigured or expanded to meet changing operational demands. Discover expert strategies here.
- Energy-Efficient Motors: The integration of energy-efficient motors reduces power consumption and operational costs while maintaining high performance.
- Durable Materials: Utilizing robust materials extends the lifespan of the conveyor system, reducing maintenance needs and downtime.
- Advanced Control Systems: Incorporating smart control systems enhances precision in operation and offers features like automatic speed adjustment and fault detection. Learn about our tailored solutions.
Types of Belt Conveyor Systems
Different types of belt conveyor systems are designed to meet specific operational needs. Selecting the appropriate type is crucial for maximizing efficiency.
Flat Belt Conveyors
Flat belt conveyors are the most common type and are ideal for transporting goods of various sizes. They are widely used in manufacturing and assembly lines. The flat surface ensures stable movement of products without slipping. Explore advanced guides and tips.
Cleated Belt Conveyors
These conveyors are equipped with vertical cleats, which prevent materials from slipping back on inclines. Cleated belt conveyors are perfect for moving bulk materials upwards or downwards at steep angles.
Inclined/Declined Belt Conveyors
Inclined and declined belt conveyors are designed to transport products between different levels. They are especially useful in facilities with limited space.
Benefits of Optimized Conveyor Systems
Implementing well-designed belt conveyor systems offers numerous advantages:
- Increased Throughput: Efficient conveyor designs facilitate faster movement of goods, leading to higher productivity.
- Reduced Operational Costs: By minimizing energy consumption and maintenance requirements, businesses can significantly lower operational expenses. Find out more about this approach.
- Improved Safety: Advanced safety features reduce the risk of accidents, ensuring a safer working environment for employees.
- Flexibility in Operations: Customizable conveyor systems allow for seamless adaptation to changing production needs.
Conclusion
Selecting the right belt conveyor design is crucial for optimizing the efficiency of material handling operations. By understanding the various designs and their specific benefits, businesses can make informed decisions that align with their operational goals. Whether opting for modular systems, energy-efficient motors, or advanced control systems, the right choice can lead to significant improvements in productivity and cost-effectiveness. For further insights and expert guidance on belt conveyor systems, visit the comprehensive resource available here.